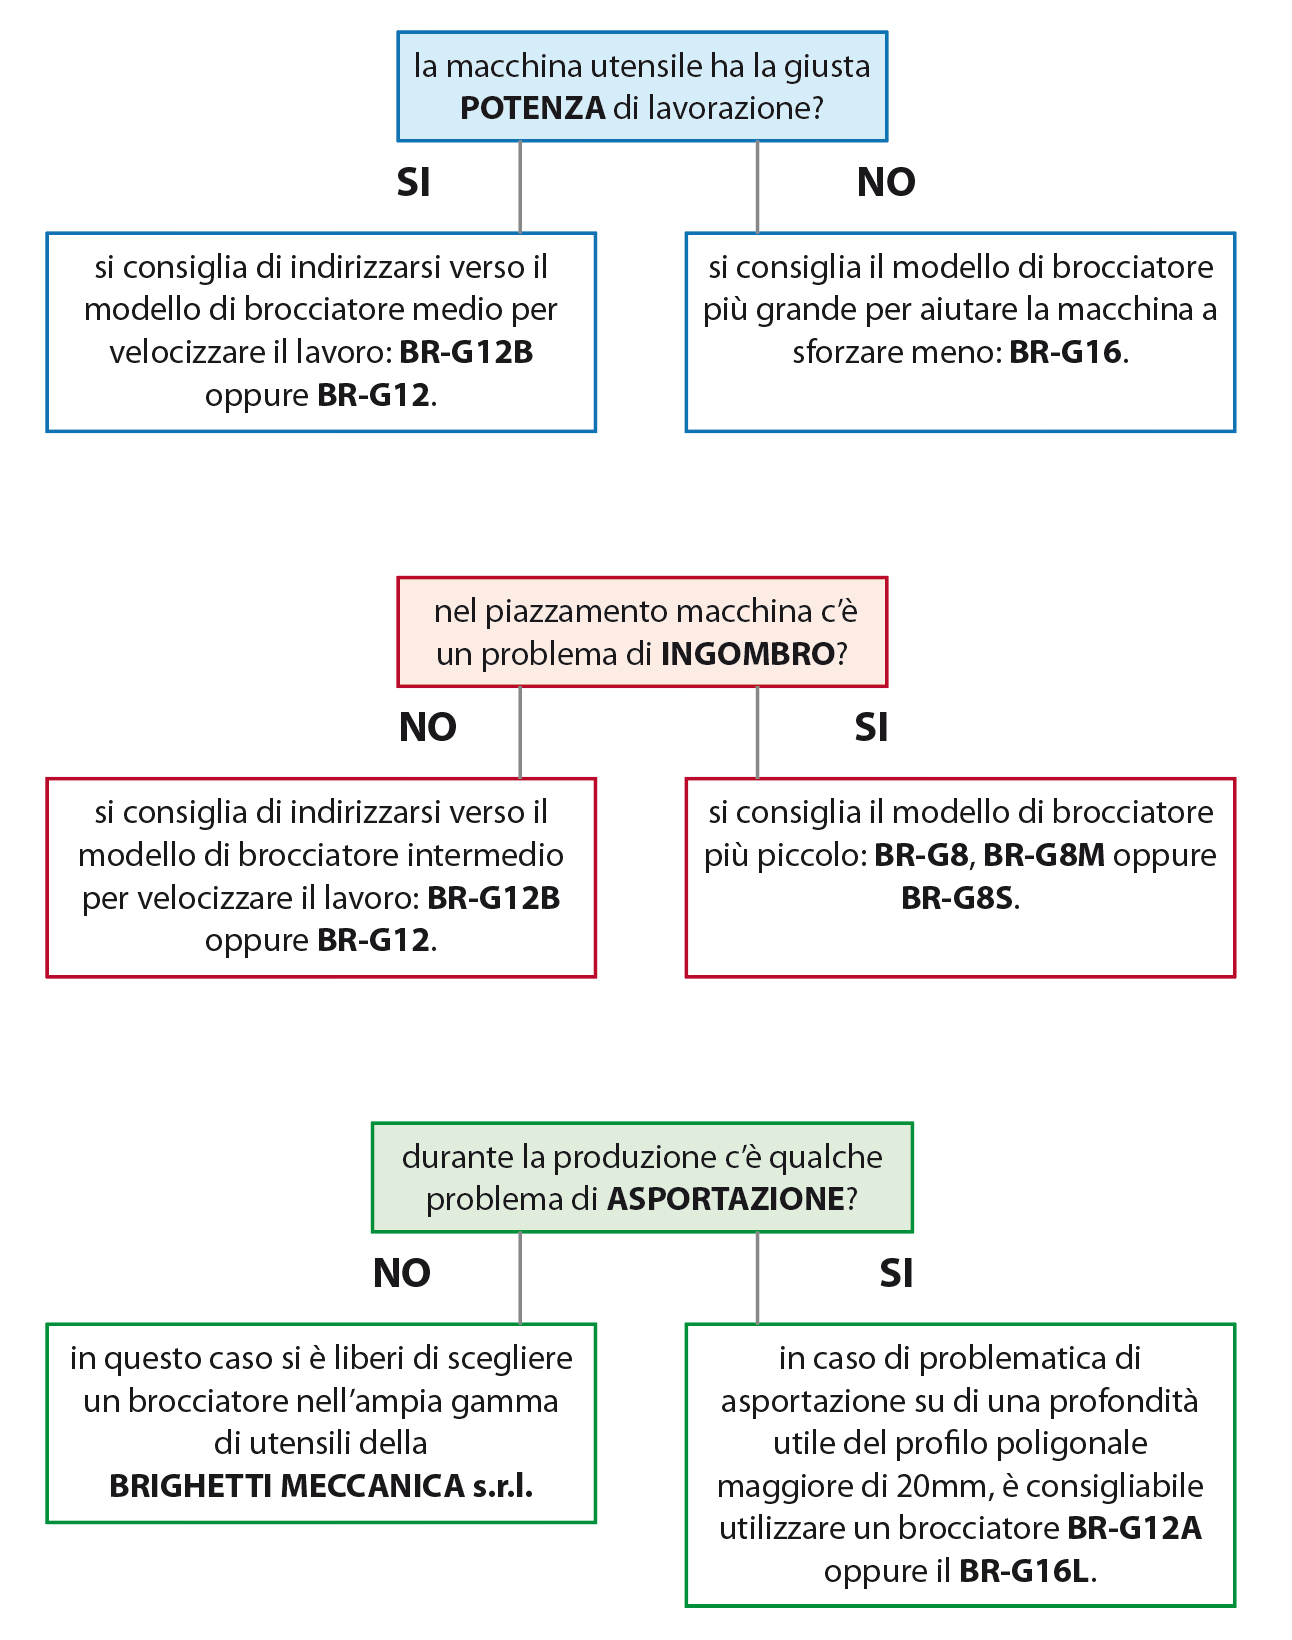
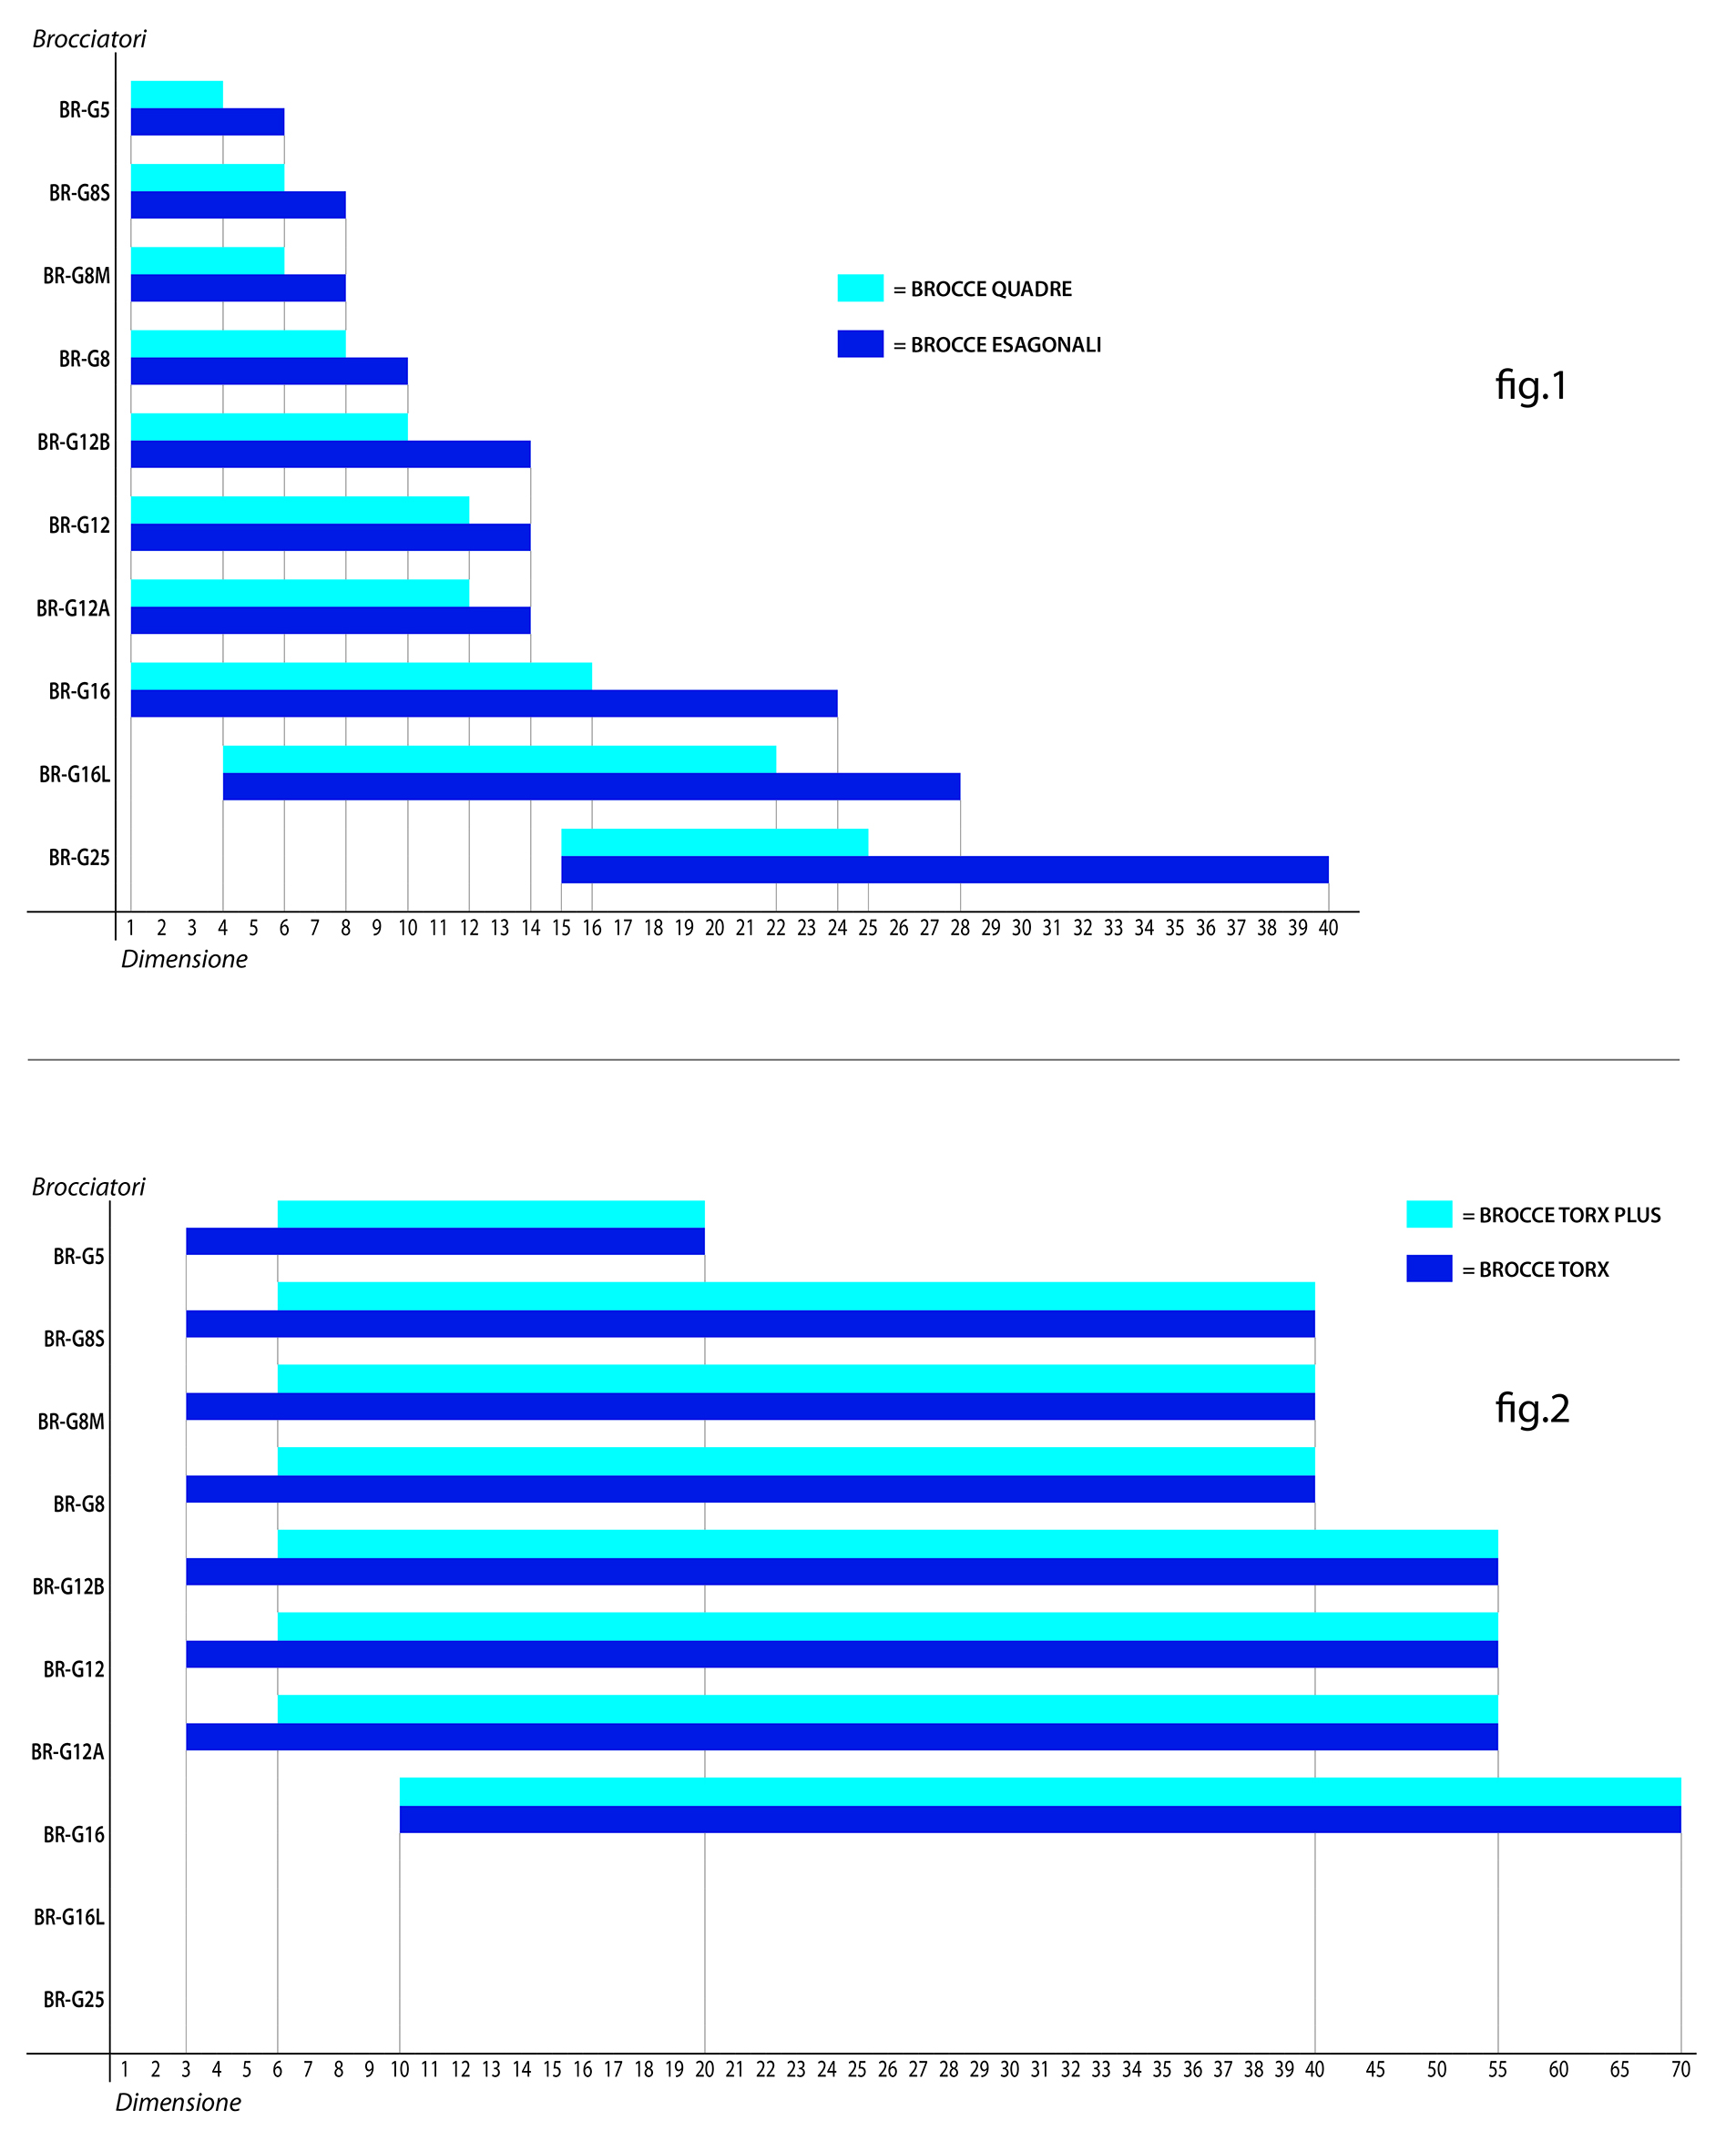
The overall dimensions of the broaching machine and broach vary depending on the type of broaching machine and can be:
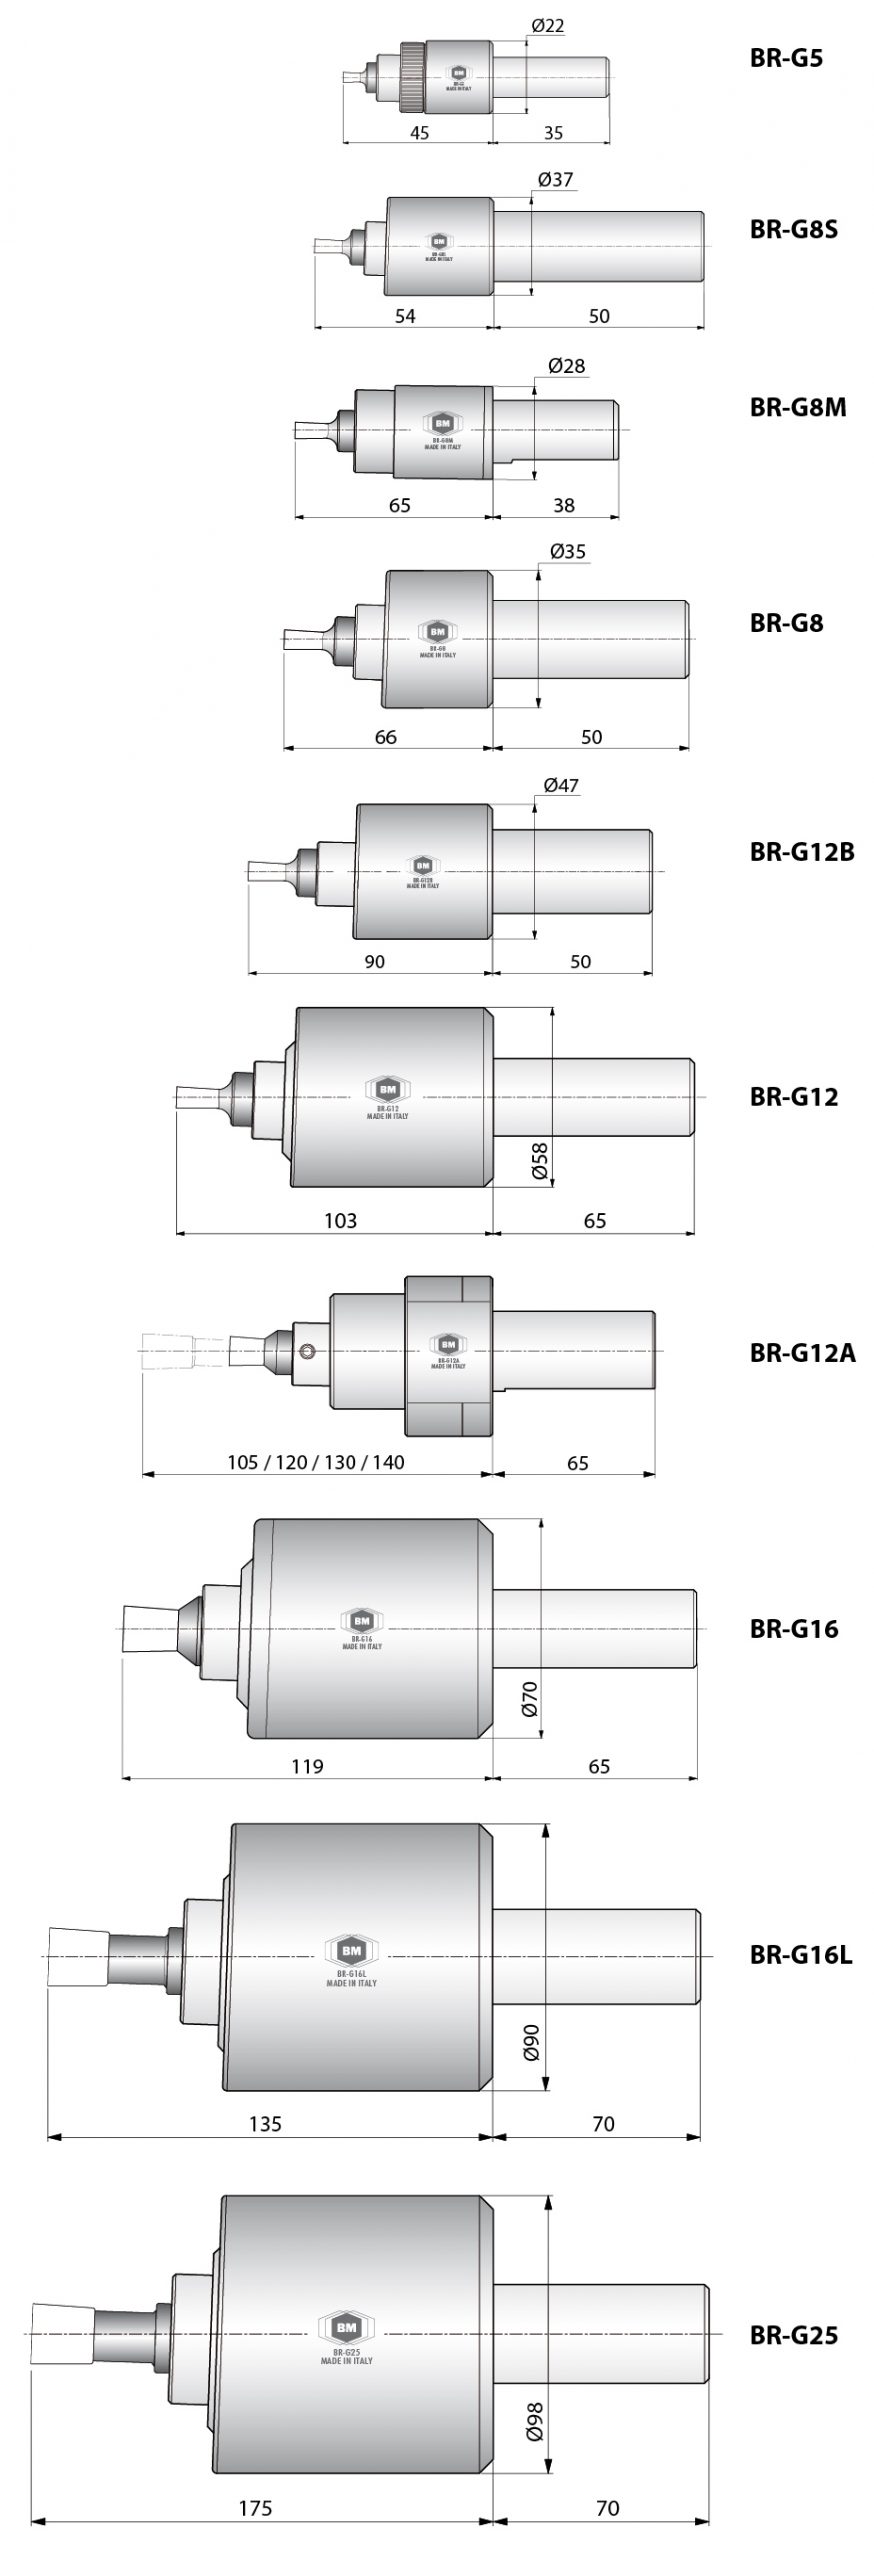
The overall dimensions of the broaching machine and broach vary depending on the type of broaching machine and can be:
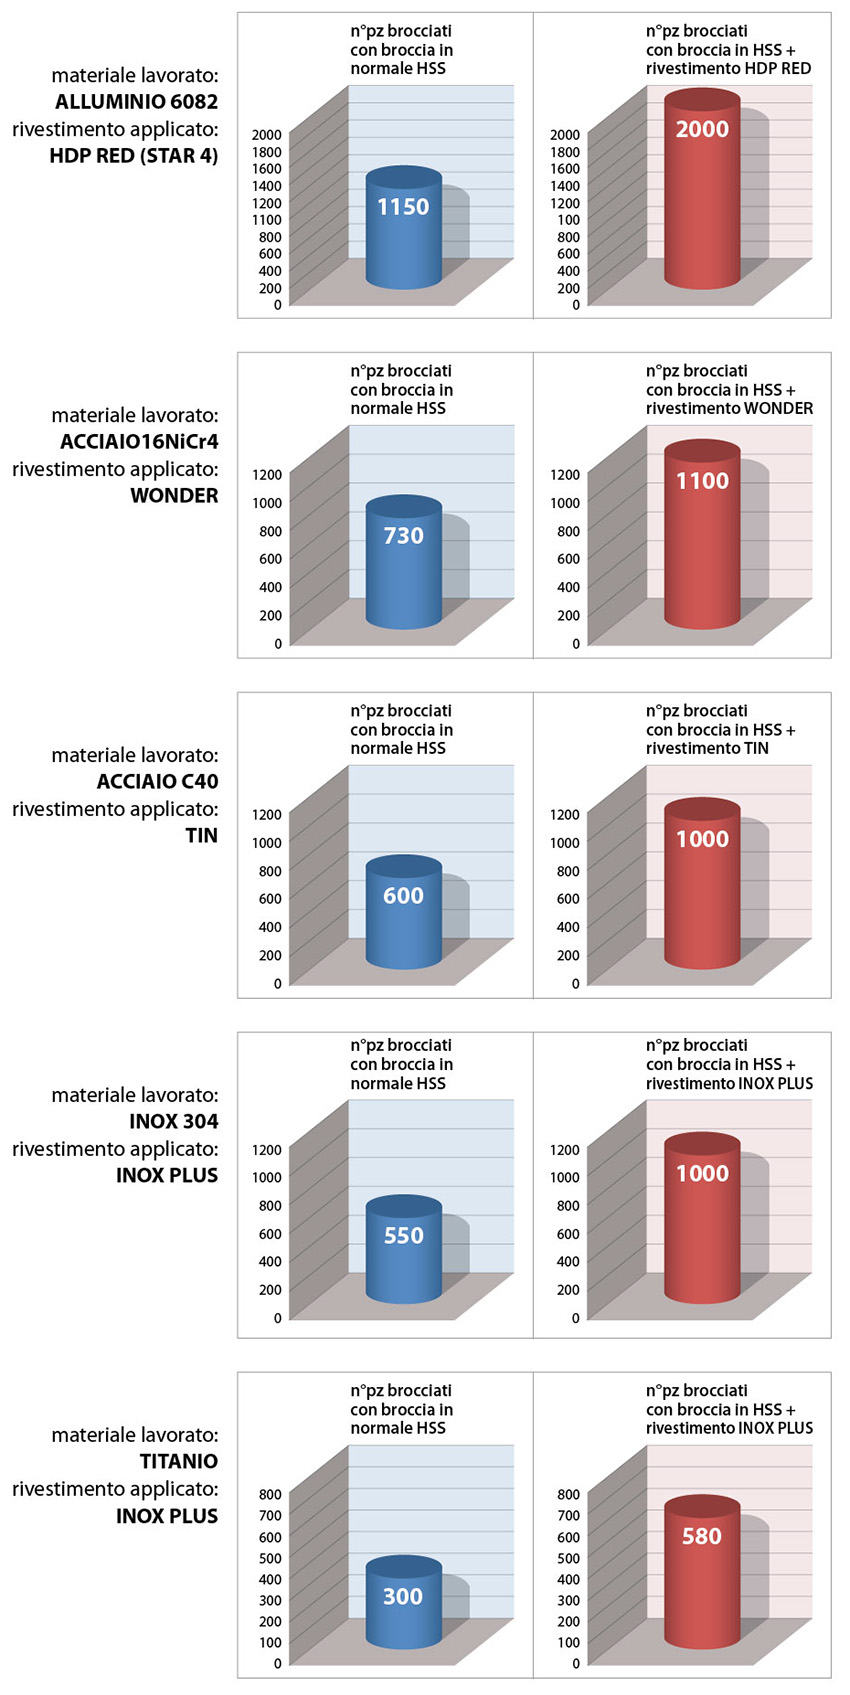
The service life of Brighetti tools depends on the conditions of use (whether proper or not), the characteristics of the material to be machined, and the amount of material removed based on the cut to be made.
Tips for Ensuring a Longer Broach Life
1) Use a machine tool that is sufficiently rigid to withstand strong axial forces that can cause vibrations and/or deflection.
2) Longer tool life can be achieved by regularly checking the tool’s cutting edge and, if necessary, performing light face regrinding before the edges become excessively worn.
Regrinding can be performed flat (zero rake angle).
As the tool is resharpened, the profile dimension gradually decreases, by approximately 0.01 for every tenth of a millimeter removed. Conversely, dies for external profiles have a cutting edge section that gradually increases.
Since the cutting axis must remain concentric with the workpiece axis, the tool’s projection from the broaching machine’s support surface must remain constant at:
– 45 mm for the G16L
– 25 mm for G12 and G16
– 18 mm for G8
– 10 mm for G5
If the resharpening exceeds 1 mm, this must be compensated for by mounting a ground washer on the tool shank to restore this dimension.
TYPES OF SHARPENING AVAILABLE UPON REQUEST, DEPENDING ON THE TYPE OF MATERIAL TO BE PROCESSED
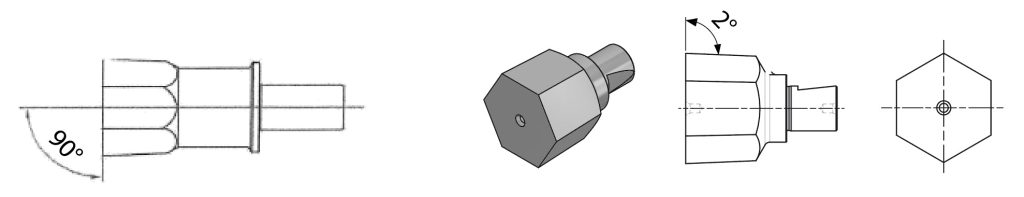
STANDARD SHARPENING “Brighetti Meccanica”
Sharpening with a flat surface and a 2° rake angle.
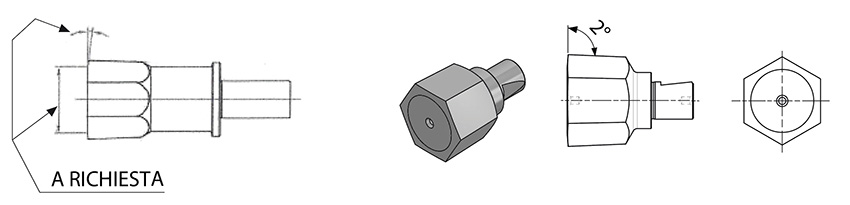
CUP SHARPENING
Sharpening on request for non-ferrous materials and stainless steels with Rm less than 900N/mm2 with a 2° rake angle.
FLAT GRINDING PERPENDICULAR TO THE CUTTING EDGE
Custom grinding for cast iron and stainless steels with a tensile strength (Rm) greater than 900 N/mm² and a rake angle of 2°.
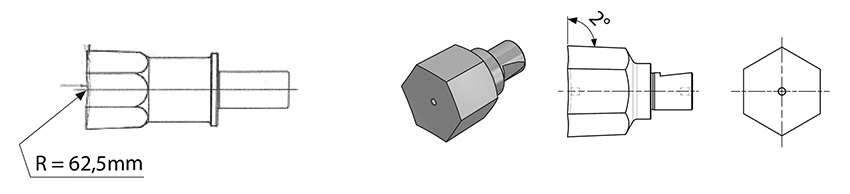
When machining square slots, it is important to remember that the amount of material to be removed is nearly double that of a hexagonal slot, so the thrust required is greater. These operations typically require very rigid machines with considerable power.
If possible, especially for square holes larger than 20 mm, certain precautions should be taken:
1) The pilot hole should always be as large as possible
2) Whenever possible, it is recommended to request that the edges be chamfered to remove the sharp edge, which is the tool’s most fragile point (see“CUSTOM SHARPENING OPTIONS THAT PROTECT DRILLS FROM WEAR”)
3) If a square cross-section with all four full faces is required, a UT-SQ counterbore can be used.
Of course, the same considerations apply to the production of large hexagonal holes, typically larger than 26 mm.
TYPES OF SHARPENING METHODS THAT PROTECT REAMERS FROM WEAR
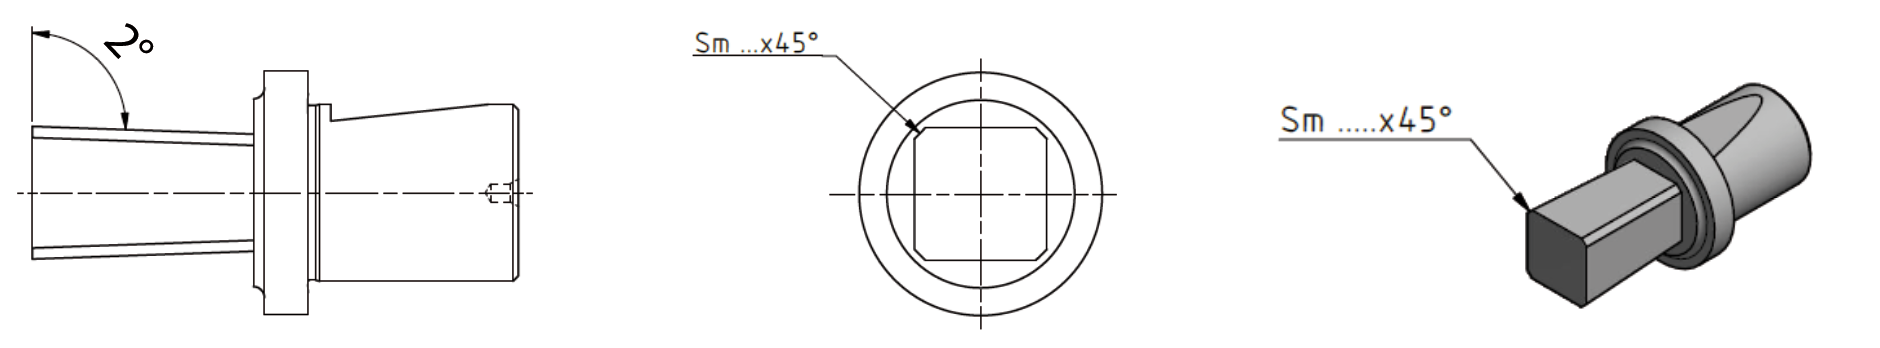
To prevent or remedy possible breakage or chipping of the edges due to the material’s hardness, reamers can be sharpened as shown in the following figures:
EDGES WITH RADIUS
square / hexagonal profile
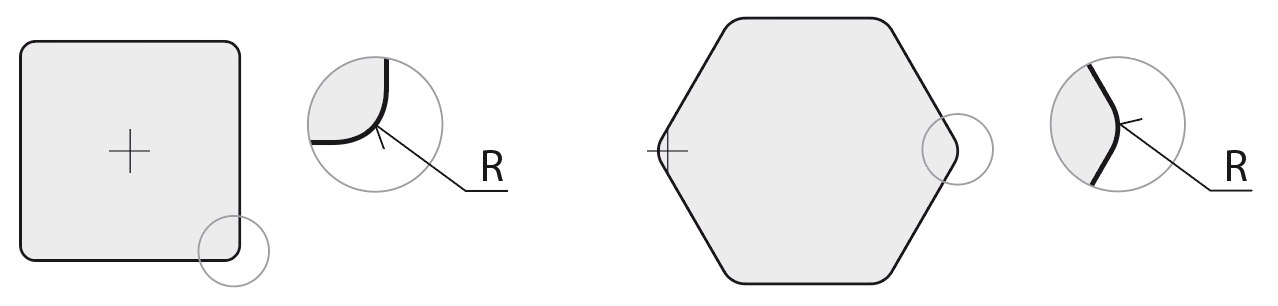
Square reamer with ROUNDED EDGES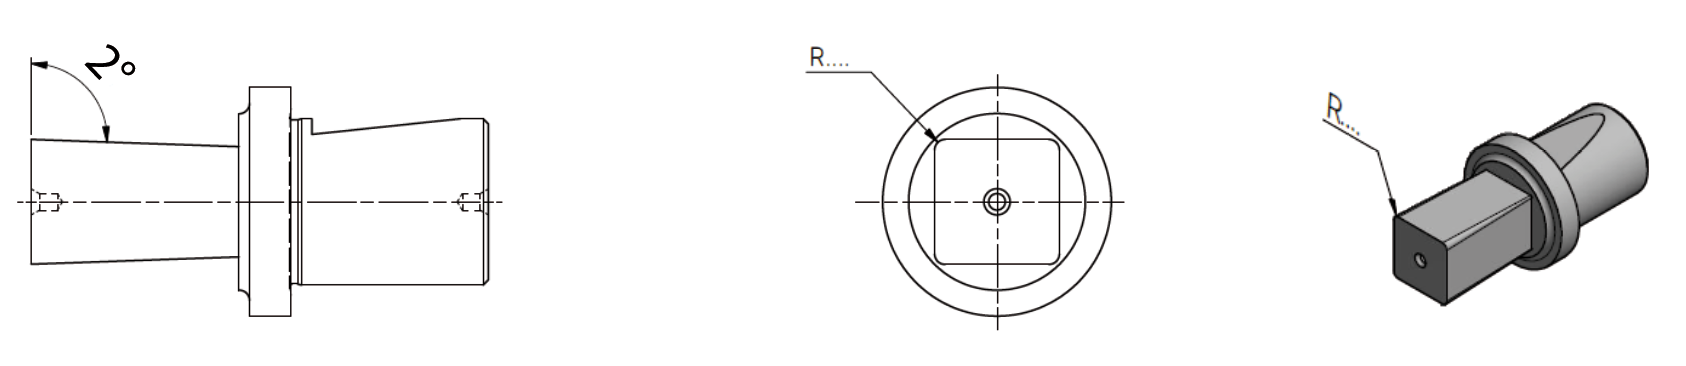
EDGES WITH GRINDED DIAMETER
square / hexagonal profile
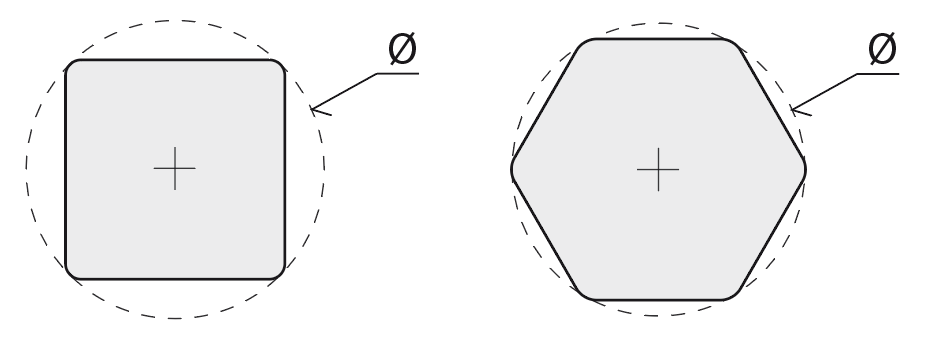
Square broach with GRINDED EDGES
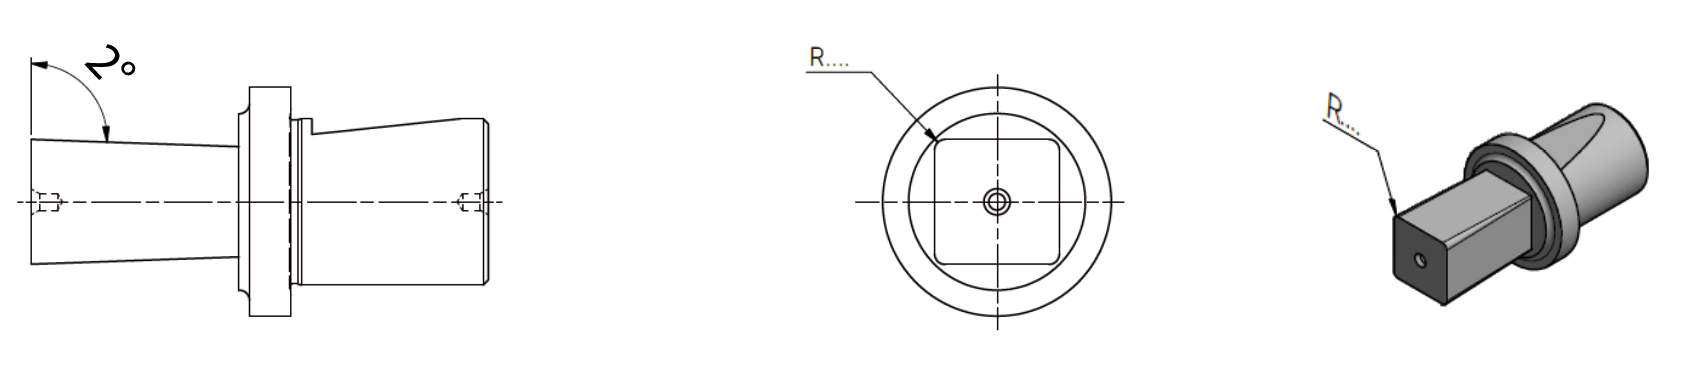
ROUNDED EDGES
, square/hexagonal profile
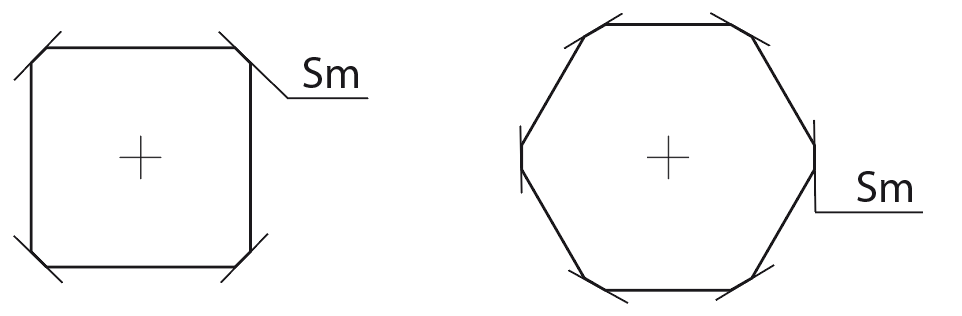
Square broach with CHAMFERED EDGES
SPECIAL PROFILE MACHINING
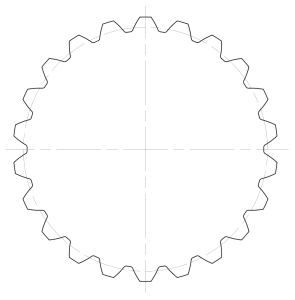
1 – EVOLVING TOOTHING (e.g., DIN 5480):
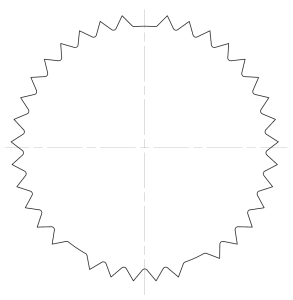
2 – MISSING TEETH:
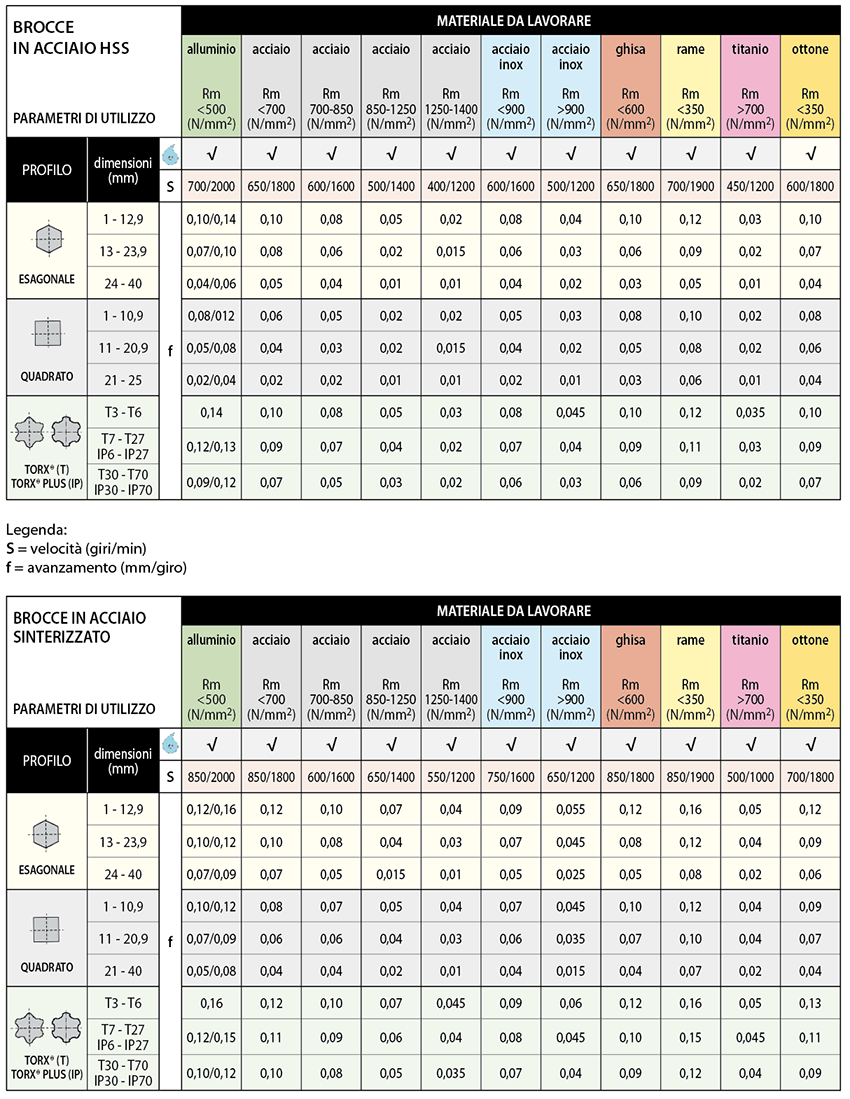
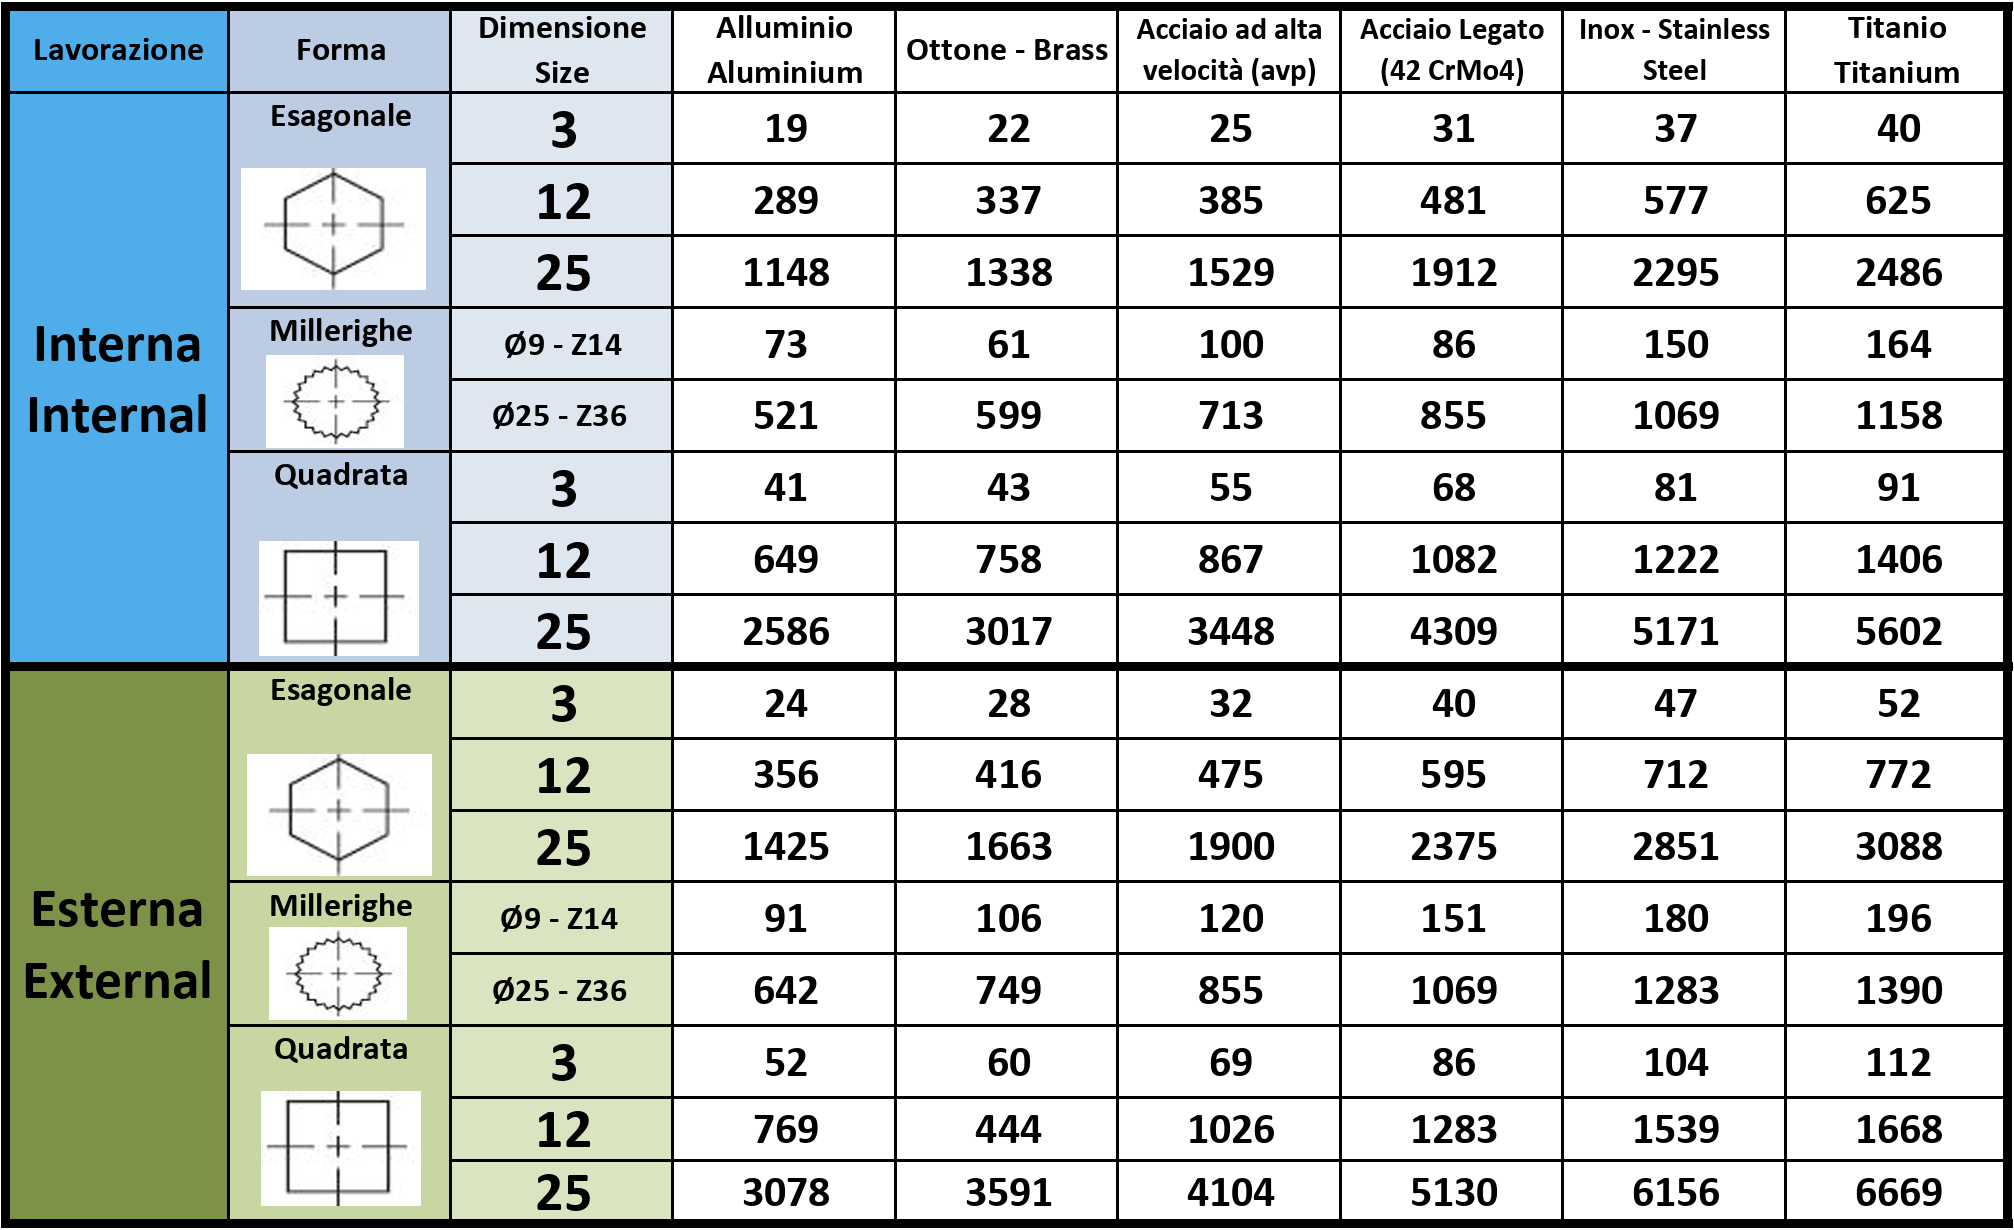
The table is provided as a reference for comparing workloads among different shapes, sizes, and materials.
The values take into account the correct machining procedure (pilot hole, chamfer, pilot hole depth, etc.).
To convert to kW, note that 1 kW = 102 kgf*m (approximately)
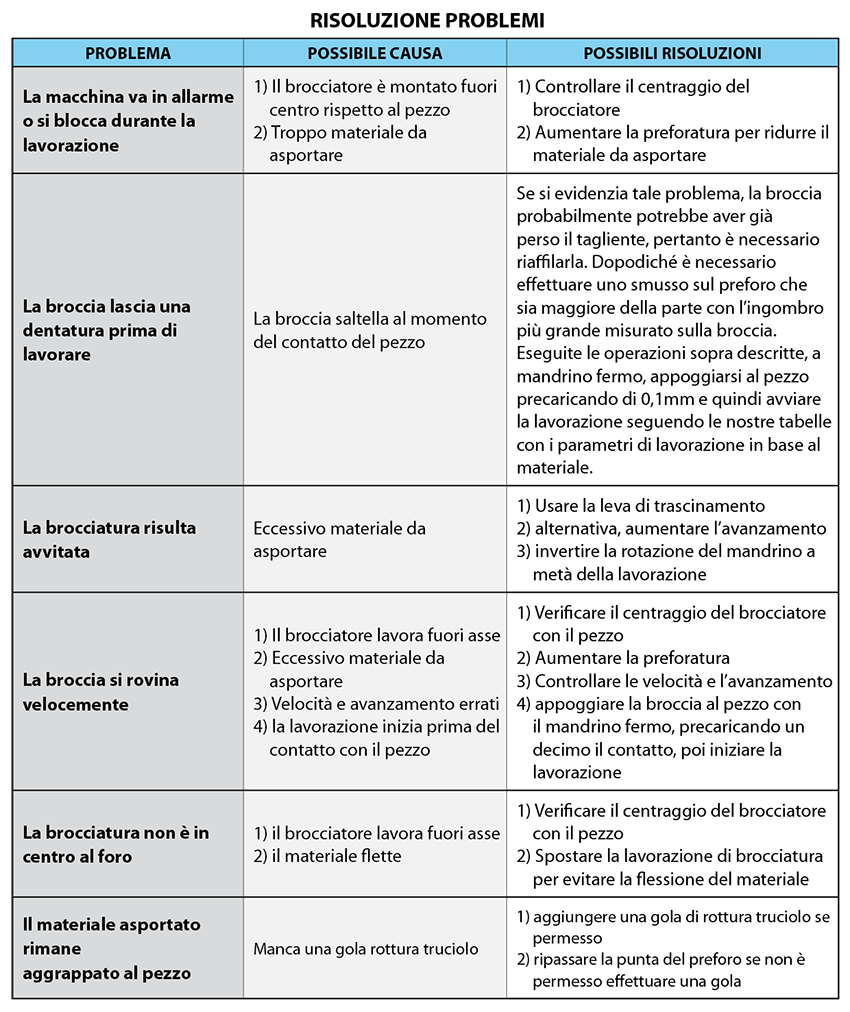
Here are some tips for troubleshooting problems during machining: